Zinc Die Casting Mold Design and Tooling Review
Prepare your design for tooling with a review of parting lines, draft, cores and visible surfaces. Plan CNC engraving, trial parts and revision approval.
Discuss your requirements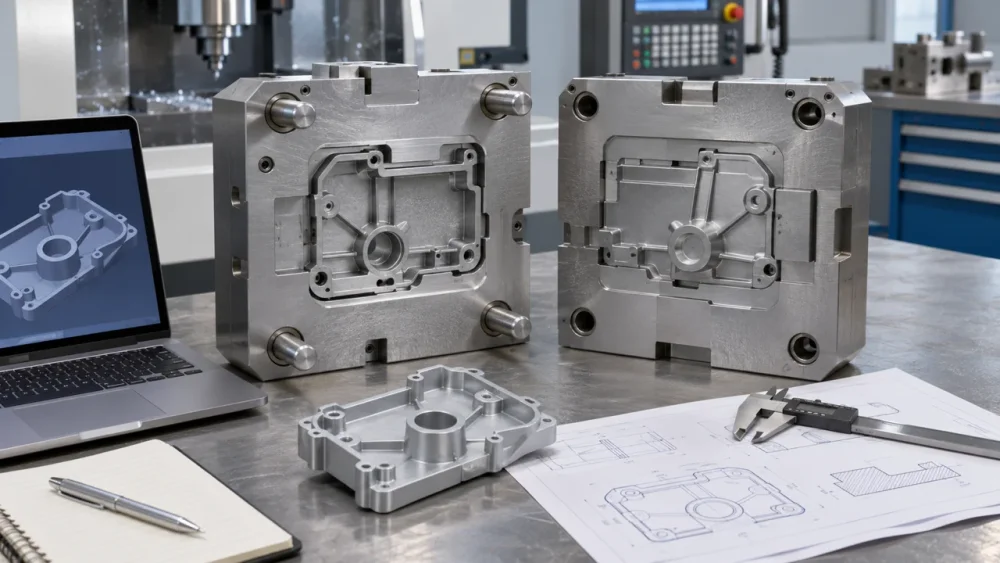
Tooling turns the approved product definition into geometry for repeatable metal parts. Gairun’s mold development and CNC engraving connect artwork or component geometry with filling, opening, extraction and finishing.
Before release, identify functional and cosmetic priorities. Manufacturing improvements must preserve the product’s intended function and appearance.
What should be agreed before paying for a mold?
Part definition
Connect the tool proposal to the approved drawing revision, geometry and supplied condition, including parting, extraction and later operations.
Trial and correction scope
Confirm whether the price includes design revisions, trial parts and agreed corrections.
Ownership and future use
Define ownership, storage, maintenance and the procedure for later changes. These terms cannot be inferred from sample approval.
A product model is not a finished tool design
| Input | What tooling review must add |
|---|---|
| Product model | Forming, shrinkage, extraction, gates, trimming and finishing requirements, including where production marks may appear. |
| Decorative artwork | Raised and recessed geometry with approved relief heights where dimensional detail controls appearance. |
| Functional component model | A dimensioned drawing with datums, tolerances, material and critical characteristics. A 3D file alone leaves acceptance incomplete. |

Parting lines, draft and extraction
Parting lines
Locate the tool split with regard to trimming and use of the surface. Hidden faces, polished display faces and sealing interfaces need different treatment.
Draft
Set release taper for the feature depth, surface and production route. One angle is not a universal rule.
Undercuts
Review moving cores, separate pieces or later machining. A modest geometry change may allow straight extraction while preserving function.
Ejection
Position contact points for wall strength, appearance and later operations; assess witness marks according to actual surface use.
Cores, gates and visible surfaces
- Cores: internal openings must fit practical tooling limits. Long or poorly supported features can complicate filling and tool life.
- Gates: agree where metal enters and where separation or finishing marks are acceptable. Identify restricted visible and functional surfaces.
- Venting and thermal balance: review walls and thick transitions as a connected casting because they solidify differently.
Review walls, ribs and transitions before geometry becomes expensive to change.
CNC engraving and trial tooling
Prepared geometry
CNC engraving creates relief, outlines and text from the approved digital model and toolmaker’s production definition.
Separate machining scope
Tool engraving and machining finished parts to functional tolerances require different equipment, fixtures and verification. Specify secondary part machining explicitly.
Physical trial
Evaluate filling, release, detail and finishing before approving the tool for the intended production route.
Review the first physical article
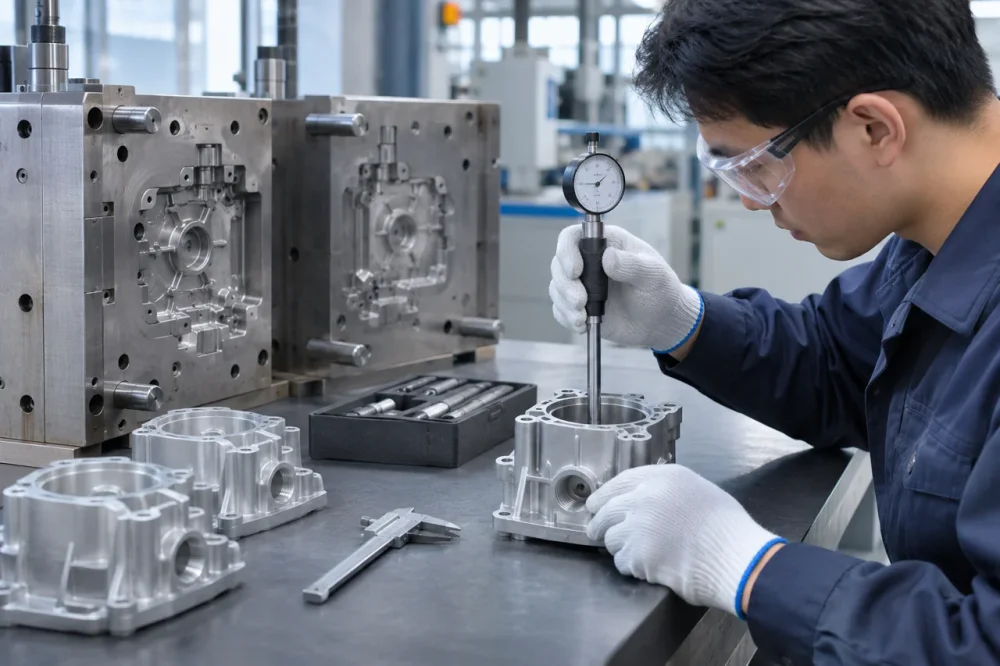
- Check against controlled requirementsCompare the first article with the drawing and intended assembly. Measure critical fit and function, and inspect identity-defining surfaces.
- Inspect the supplied conditionInclude dimensional effects of decoration or finishing. A raw casting inspection may only cover part of acceptance.
- Follow the productMedals may prioritize relief, borders and attachments; housings may prioritize mounting datums and mating surfaces.
- Record measurable correctionsDefine references for requests such as sharper or deeper features. Link the approved revision, sample record and tool changes.
Agree ownership and revision controls
| Agreement | What to confirm |
|---|---|
| Commercial terms | Ownership, storage, maintenance and conditions of future use. A tooling charge alone does not establish these terms. |
| Design changes | Evaluation and pricing of local rework, new tooling or a different process. Small drawing changes may affect connected features. |
| Repeat orders | Tool identity and approved part revision. Reassess suitability if the finish or attachment changes. |
Keep tooling and recurring production scope separate using the sourcing guide.
Prepare files for tooling review
- Model or artwork, dimensioned drawing, material preference and intended quantity.
- Marked critical interfaces, visible faces and surfaces that cannot carry tooling or finishing marks.
- Mating parts where needed to explain the design.
- Sample and inspection evidence required before production approval.
Review the quality records, then request a tooling review to agree geometry, production route and approval responsibilities before the tool is made.
